Why parboiled mills need stage tracking
In a raw-rice mill, paddy goes into the huller and rice comes out the same day. A parboiled mill is different. Paddy is soaked for hours, steamed, dried in the sun or a drier, tempered and only then milled. Each step takes time, uses fuel and labour, and loses weight. When the season's outturn is lower than expected, the owner needs to know which stage lost it – and on whose shift.
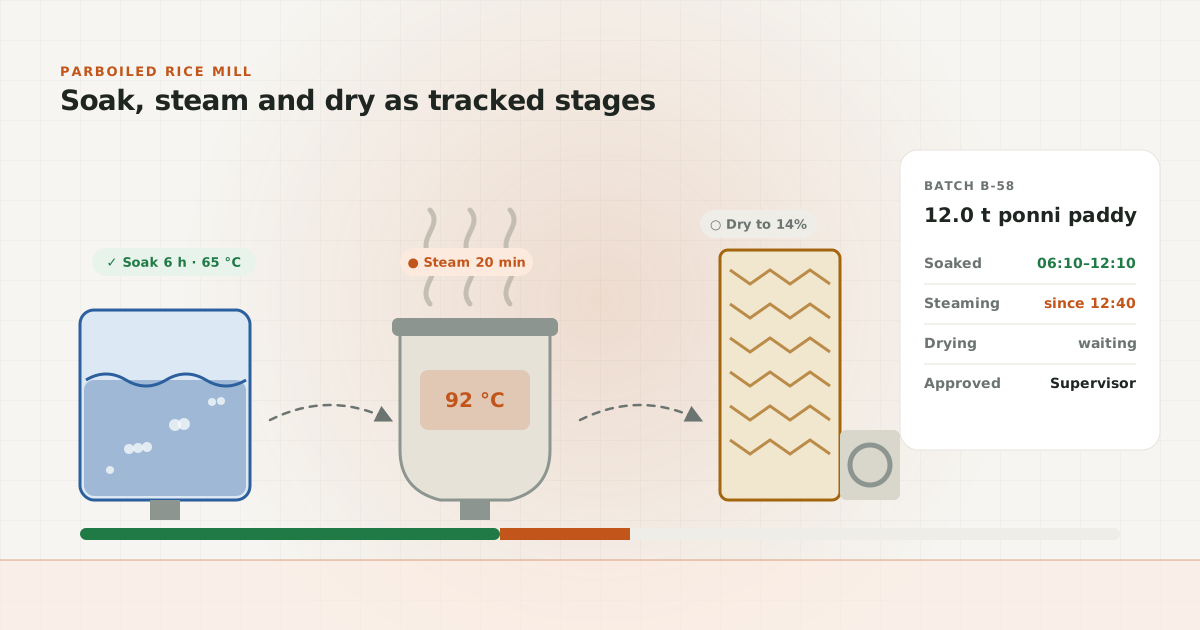
Grano treats parboiling as a route of stages you define. A typical route is soak → steam → dry → mill → sort → pack, but you can add or rename stages to match your plant. Every batch carries its own copy of the route, with the people responsible and a due date for each step.
What each stage records
- Quantity in and quantity out, so loss is measured rather than assumed.
- By-products taken out at that stage – broken, bran and husk at milling, for example.
- Who did the work, when it started and when it was submitted.
- Approval or return by a supervisor, with a note when it is sent back.
Because the supervisor's approval is recorded, disputes about moisture or colour after drying have a written answer. Because loss is recorded at each stage, outturn by stage becomes a report rather than an argument. As an illustration, if drying usually loses a fixed share of weight and one week it loses noticeably more, that shows up against that stage and that week – not in a stock mismatch three months later.
From batch to bag
When milling is approved, the batch produces a rice lot linked back to the paddy lots that went in. Packing turns that lot into bags of the sizes you sell, records damaged or rejected bags and uses bag stock from the godown. The lot page then tells the full batch story: which loads of paddy, which stages, which people, and which bags came out. When a buyer asks where a consignment came from, the answer is on one screen.
Machines matter as much as people in a parboiled plant. Boilers, driers and rubber rolls can be listed as machines with service schedules; a breakdown is logged as a task on that machine, with downtime recorded. Over a season, that shows which equipment is costing you batches.
Stages can also carry tasks. A supervisor can give a person or a team a piece of work linked to a batch or a stage – check the boiler pressure, re-dry a batch that came back damp – with a due date and an optional review. Each person sees their own list under My work, and the assignment reaches them on WhatsApp, so the shed does not depend on someone remembering a phone call.
Process stages, packing and maintenance are part of the Pro plan, from ₹9,999/month, and every screen works in English, Tamil and Hindi on an ordinary Android phone in the shed.
How do you measure loss in parboiling?
Parboiled outturn is still rice out divided by paddy in, on the dry paddy that entered the batch. The difference is that weight moves up and down on the way. Paddy takes on water in the soaking tank, holds it through steaming and gives it back in the drier. So the useful comparison is not between two wet weights. It is between the dry paddy that went in and the dried paddy that comes out of the drier, and then between that and the milled rice.
A worked example. A batch starts with 12,000 kg of paddy. After soaking, steaming and drying, 11,700 kg of dried paddy goes to the huller – a drying-stage loss of 300 kg, or 2.5%. Milling gives 8,040 kg of rice and broken, plus bran and husk. Rice outturn on the original paddy is 67%. If the next batch of the same variety loses 4% in drying, the gap shows up against the drying stage and that shift, and the supervisor can check the drier temperature or the time in the yard.
Grano does the arithmetic from the quantities each operator records. What the plant has to do is weigh at the same points every time – usually into the tank and out of the drier – so batches can be compared.
A day in a parboiling plant with stage tracking
The night shift soaks two batches and submits the soak stage with quantity in and the time it went into the tank. In the morning the supervisor sees both on his phone, approves one and returns the other with a note that it went in late. The steaming operator picks up the approved batch, records the start and end, and submits. In the afternoon the drier operator records the dried weight. The owner, without calling anyone, can see which batches are in the tank, which are steaming, which are drying and which are overdue.
When the boiler trips, the operator logs a breakdown on that machine. The downtime is recorded, the maintenance person gets the task on WhatsApp, and the delayed batches carry the reason in their timeline.
Common mistakes when setting up stages
- Too many stages on day one. Start with soak, steam, dry and mill; add tempering or sorting once people are used to submitting.
- Weighing at different points on different shifts. Agree where each stage is weighed and write it on the stage name if needed.
- Every stage approved by the owner. Give approval to the shift supervisor so batches do not wait for one person.
- Mixing lots in a tank without recording it. Pick all the paddy lots that go into a batch, so the batch story stays true.
- Skipping by-products at milling. Without broken, bran and husk, the loss figure is wrong and outturn cannot be trusted.